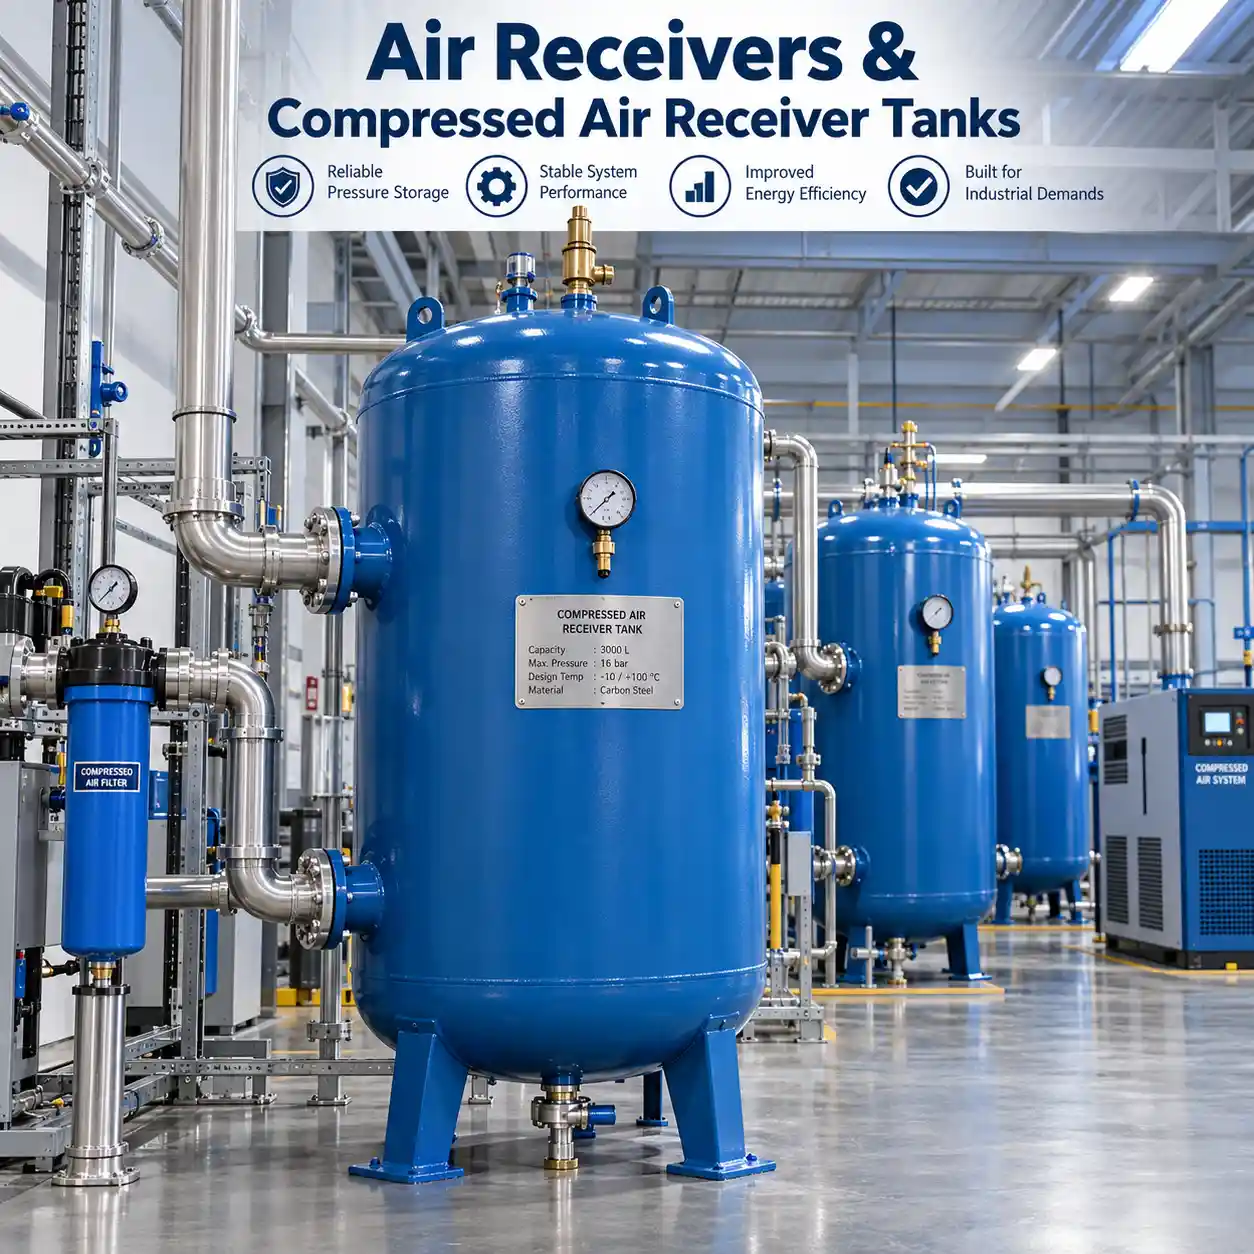
AIRNOVEX supplies industrial air receivers, vertical and horizontal compressed air receiver tanks, and custom storage solutions for compressor systems. Request a quote.
For specifications, availability or a quotation, please share your
required quantity, application and destination country.
Industrial Air Receivers for Stable Compressed Air Supply
Air receivers provide compressed air storage between the compressor and the plant air system. The added storage volume helps absorb short-term changes in demand, supports pressure stability and provides reserve air for equipment with intermittent peak consumption.
AIRNOVEX supplies compressed air receiver tanks for industrial compressor rooms, factory utilities, OEM machinery and engineered compressed air systems. Vertical, horizontal and project-specific configurations are available to match compressor airflow, operating pressure, installation space and piping requirements.
Primary FunctionCompressed Air Storage
OrientationVertical / Horizontal
Typical UseIndustrial Compressor Systems
SupplyStandard & Custom Projects
What is an air receiver?
An air receiver is a pressure vessel that stores compressed air at system pressure. It acts as a buffer between compressor output and changing plant demand, allowing stored air to cover short-duration demand peaks while the compressor continues operating within its normal control range.
System Performance
What an Air Receiver Does in a Compressed Air System
Industrial air demand is rarely constant. Pneumatic cylinders, blow-off operations, packaging equipment, production tools and automated machines can create short periods of high airflow. Receiver storage helps the system respond to those changes without relying on the compressor to react instantly to every demand fluctuation.
01
Provides Stored Air
A compressed air storage tank holds reserve air that can supplement compressor output during short periods of increased demand.
02
Stabilizes System Pressure
Additional storage volume slows rapid pressure changes and can improve pressure stability at downstream equipment.
03
Supports Compressor Control
Correctly sized storage can reduce unnecessarily rapid compressor loading, unloading or start-stop activity, depending on the control method.
04
Handles Peak Air Demand
Processes with short, high-flow events can draw from stored air instead of forcing the compressor to be sized only around a momentary peak.
05
Collects Condensate
When hot compressed air cools inside a receiver, part of its water vapor may condense. Proper drainage allows the collected liquid to be removed.
06
Adds Useful System Volume
Greater system volume gives compressor controls more time to respond when air consumption changes, which can improve overall operating stability.
Engineering note: An air receiver improves storage and pressure response, but it cannot compensate for a compressor that is undersized for continuous demand, excessive piping pressure loss or unresolved compressed air leaks.
Receiver Location
Wet Receiver, Dry Receiver or Point-of-Use Storage?
Receiver location determines how the stored air is used. Larger compressed air systems may use more than one receiver: one near the compressor, another after air treatment, and additional storage near equipment with unusually high intermittent demand.
Typical air receiver locations in an industrial compressed air system
Receiver Position
Typical Location
Main Purpose
Important Consideration
Wet Air Receiver
Before the compressed air dryer
Provides compressor-side storage and allows part of the moisture carried by hot compressed air to condense as the air cools.
Condensate drainage is important because liquid water can accumulate inside the vessel.
Dry Air Receiver
After the dryer and filtration system
Stores treated compressed air and provides reserve capacity for downstream plant demand.
Capacity should reflect usable storage between the system's upper and lower operating pressures.
Point-of-Use Receiver
Close to a high-demand machine or production process
Supplies local short-duration airflow and reduces dependence on moving the entire peak flow through long distribution piping.
Useful when one machine has intermittent demand that is much higher than its average consumption.
Tank Configuration
Vertical, Horizontal and Custom Air Receiver Tanks
Tank orientation is generally selected according to available space, equipment layout and piping arrangement rather than storage performance alone.
Space-Saving Layout
Vertical Air Receiver Tank
A vertical air receiver tank uses floor space efficiently and is commonly installed beside industrial air compressors, dryers and filtration equipment.
Smaller floor footprint
Common in compressor rooms
Suitable for centralized plant air systems
Practical where adequate ceiling height is available
Low-Profile Installation
Horizontal Air Receiver Tank
A horizontal air receiver tank is often selected where installation height is restricted or when the vessel needs to fit into a skid, equipment platform or OEM package.
Reduced overall installation height
Suitable for skid-mounted systems
Useful for OEM machinery packages
Flexible connection arrangement
Project-Specific Design
Custom Air Receiver Tanks
AIRNOVEX can review custom receiver requirements for engineering companies, distributors, OEM customers and compressed air system integrators.
Project-specific storage capacity
Connection and nozzle arrangement
Vertical or horizontal configuration
Surface finish and color requirements
OEM labeling and equipment integration
Technical Data
Industrial Air Receiver Technical Specifications
The correct specification depends on compressor capacity, operating pressure, site conditions and the requirements of the destination market. The values below represent common industrial project ranges rather than a fixed specification for every AIRNOVEX air receiver.
Typical configuration options — final data should be confirmed for each project.
Parameter
Typical Configuration / Selection Basis
Product Type
Industrial air receiver / compressed air receiver tank / compressed air storage tank
Capacity Range
Common project requirements range from approximately 100 L to 10,000 L. Other capacities can be reviewed according to system requirements.
Working Pressure
Selected according to compressor and plant operating pressure. Many industrial applications operate within approximately 8–16 bar, subject to final vessel specification.
Design Pressure
Defined according to maximum system conditions, required design margin and applicable pressure-vessel requirements.
Material
Carbon steel is commonly used for general industrial compressed air service. Alternative material requirements can be reviewed for specific applications.
Tank Orientation
Vertical or horizontal
Surface Treatment
Industrial protective coating. Project-specific finish, coating system and color can be discussed during technical confirmation.
Operating Temperature
Specified according to compressor discharge conditions, receiver position and site environment.
Inlet / Outlet Connection
Selected according to compressor airflow, receiver capacity and compressed air piping design.
Drain Connection
Configured according to vessel design. Manual or automatic condensate drainage can be considered as part of the system layout.
Applicable Compressor Power
Receiver sizing should be based primarily on compressor airflow, demand profile and pressure range rather than motor kW or HP alone.
Documentation
Technical documentation requirements are confirmed according to project scope and destination market.
Certification / Code
Any required pressure-vessel code, certification, inspection or third-party documentation must be specified during quotation and confirmed before manufacturing.
Final volume, dimensions, pressure rating, material, nozzle arrangement, wall thickness, inspection, testing and documentation depend on the approved project specification.
Engineering Selection
How to Size an Air Receiver for an Industrial Compressor System
There is no single receiver size that is correct for every compressor of the same horsepower. Useful storage depends on compressor airflow, pressure range, demand fluctuations and how the compressor is controlled.
Compressor Airflow
Start with actual delivered airflow in CFM, m³/min or m³/h. Airflow provides a better sizing basis than motor power alone.
Pressure Range
Define the maximum storage pressure and the minimum pressure the process can accept. The difference between these pressures determines how much stored air is usable.
Peak Demand
Identify equipment that requires high airflow for several seconds or minutes. These intermittent loads often have the greatest effect on receiver sizing.
Compressor Control
Load/unload, start/stop, variable speed and multi-compressor systems respond differently to storage volume and pressure changes.
Piping & Pressure Drop
An adequately sized receiver cannot correct restricted piping. Pipe diameter, distance and peak airflow should be checked together with storage requirements.
Future Demand
If additional production equipment is expected, future airflow and storage requirements should be considered before the receiver and piping layout are finalized.
Quick Storage Estimate for Intermittent Demand
For an initial engineering check, the receiver volume required to cover a short airflow deficit can be estimated from the airflow demand, duration and allowable pressure drop:
V ≈ (Q × t × Patm) / (P1 abs − P2 abs)
V = approximate receiver volume Q = additional free-air demand t = duration of the demand event P1 abs = starting absolute receiver pressure P2 abs = minimum acceptable absolute pressure
This relationship is useful for preliminary storage estimates only. Final receiver selection should also consider compressor response, system volume, pressure losses, operating margin and applicable engineering requirements.
System Diagnosis
When Additional Compressed Air Storage May Help
A larger receiver is not automatically the solution to every pressure problem. However, several operating conditions can indicate that usable storage should be reviewed.
Pressure Drops During Short Production Cycles
If system pressure is normally stable but falls when a particular machine cycles, local or central storage may help cover the temporary airflow requirement.
Frequent Load / Unload Cycling
Rapid pressure changes can cause some compressor control systems to switch operating states frequently. Additional system volume may help slow those changes.
High Intermittent Air Consumption
Large cylinders, pneumatic presses, blasting processes and blow-off operations may require far more airflow for a short period than their average consumption suggests.
Long Distance to High-Demand Equipment
A point-of-use receiver can sometimes provide a more practical buffer where a high-flow machine is located far from the compressor room.
Before increasing tank size
Check for air leaks, clogged filters, restricted piping, undersized distribution lines, incorrect pressure settings and insufficient compressor capacity. Storage should be selected as part of the complete compressed air system.
Orientation Comparison
Vertical vs. Horizontal Air Receivers
Both configurations provide compressed air storage. The better choice normally depends on the physical installation rather than a difference in basic receiver function.
Practical comparison for industrial air receiver installations
Selection Factor
Vertical Air Receiver
Horizontal Air Receiver
Floor Space
Uses less floor area for a comparable storage volume
Requires more horizontal installation space
Installation Height
Requires greater vertical clearance
Suitable where ceiling or equipment height is limited
Compressor Room
Common choice for standalone plant installations
Useful when room geometry favors a low-profile vessel
OEM / Skid Integration
Possible where package height permits
Often convenient for packaged compressor and machinery skids
Drainage
Drain normally located at the vessel's lowest point
Drain arrangement should match the vessel's lowest condensate collection point
Typical Decision Driver
Limited floor area
Limited installation height or package layout
Project Requirements
Material, Pressure Rating and Compliance Requirements
An industrial air receiver is a pressure vessel, so the required working pressure, design conditions and destination-market requirements should be identified before manufacturing.
Material Selection
Carbon steel is widely used for standard industrial compressed air service. Material selection should consider operating environment, corrosion exposure and project requirements.
Pressure Rating
The receiver must be specified for the maximum pressure conditions it can experience in service, not only the plant's typical operating pressure.
Destination Market
Pressure-vessel requirements differ by country and application. Required codes, conformity assessment, inspection and documentation should be stated in the RFQ.
For U.S. and European projects
If your project specifies ASME BPVC Section VIII, EU pressure-equipment requirements, third-party inspection or another local pressure-vessel standard, include that requirement in your inquiry. AIRNOVEX will confirm the applicable manufacturing and documentation scope before accepting the specification.
Installation Planning
Air Receiver Installation Details That Matter
Receiver performance depends on more than vessel capacity. Connection sizing, drainage, location and maintenance access all affect how well the tank integrates with the compressed air system.
Inlet & Outlet Sizing
Connections should support the required airflow without creating unnecessary pressure loss. Large receiver capacity does not compensate for undersized piping.
Condensate Drainage
Moisture can accumulate inside the vessel. The drain location should remain accessible for inspection and routine condensate removal.
Maintenance Clearance
Leave adequate space for fittings, drains, inspection points and maintenance access required by the installation.
Foundation & Supports
The mounting surface and anchoring arrangement should be suitable for vessel dimensions, operating weight and local site conditions.
Indoor Installation
Check equipment-room ventilation, available height, service access and proximity to compressors and air treatment equipment.
Outdoor Installation
Outdoor projects may require additional consideration for ambient temperature, weather exposure, coating system, corrosion protection and drainage.
Industrial Applications
Where Industrial Air Receivers Are Used
Air receivers are used in centralized compressor stations as well as near individual production equipment. The required storage capacity depends on how each facility consumes compressed air.
Manufacturing Plants
General factory air, pneumatic machinery, production tools, assembly lines and automated equipment.
Automotive Industry
Pneumatic assembly, component production, automation equipment and plant utility compressed air.
Food & Beverage
Packaging, conveying and pneumatic control systems used with application-appropriate air treatment.
Pharmaceutical Production
Utility and process-support compressed air systems with suitable downstream treatment for the application.
Textile Industry
Pneumatic controls, textile machinery, air-jet processes and centralized plant air systems.
Electronics Manufacturing
Assembly equipment, pneumatic automation, production tools and controlled manufacturing processes.
Mining & Heavy Industry
Compressor stations supporting pneumatic equipment, workshops and heavy-duty plant operations.
Construction & Workshops
Pneumatic tools, maintenance facilities, fabrication shops and site compressed air installations.
OEM Equipment
Compressed air storage integrated into machinery, compressor packages and engineered equipment skids.
B2B Supply
AIRNOVEX Air Receiver Supply for Industrial Projects
Industrial buyers often need a receiver that fits an existing compressor room, a defined piping layout or an OEM equipment package. AIRNOVEX works with distributors, engineering companies, factories and system integrators on both standard and project-specific compressed air storage requirements.
Manufacturer Direct Supply
Direct supply for industrial distributors, engineering contractors, factory projects and compressed air system integrators.
OEM Customization
Capacity, tank orientation, connections, supports, finish and labeling can be reviewed for OEM equipment projects.
System Matching
Receiver selection can be considered together with compressor airflow, pressure range, dryer configuration and downstream demand.
Technical Specification Review
Project details are reviewed before manufacturing so that critical vessel and connection requirements are clearly defined.
International Project Support
Destination market, documentation requirements, shipping information and requested pressure-vessel standards can be reviewed during quotation.
Complete Compressed Air Systems
Air receivers can be supplied together with AIRNOVEX screw compressors, VSD compressors, dryers, filters and other air compressor system components.
Buyer Guide
Questions to Resolve Before Buying an Air Receiver
How much storage does the system actually need?
Determine whether the receiver is intended mainly for compressor control, general system storage or a specific intermittent load. These uses can lead to different capacity requirements.
What is the maximum pressure?
Provide normal operating pressure as well as the maximum pressure the receiver may encounter. The required vessel rating should be based on the actual design conditions.
Where will the tank be installed?
Compressor-room dimensions, ceiling clearance, piping routes and maintenance access determine whether a vertical or horizontal receiver is more practical.
Is the receiver before or after the dryer?
Wet and dry receiver locations serve different system functions. Defining the intended position helps determine drainage and storage requirements.
Are there short-duration peak loads?
Provide the peak airflow and how long the event lasts. This is particularly important for pneumatic cylinders, presses, blow-off processes and similar equipment.
Which pressure-vessel requirements apply?
State the destination country and any required design code, inspection, certification or documentation before the quotation is finalized.
Request for Quotation
Information to Send for an Air Receiver Quote
A complete RFQ allows the receiver configuration to be checked before pricing and reduces unnecessary revisions during technical confirmation.
Compressor & Air Demand
Compressor airflow in CFM, m³/min or m³/h
Normal operating pressure
Maximum system pressure
Compressor type and control method
Peak air demand and duration, if known
Receiver Configuration
Required tank capacity, if specified
Vertical or horizontal orientation
Inlet and outlet connection sizes
Available installation dimensions
Indoor or outdoor installation
Project Information
Required quantity
Application or industry
Destination country
Requested delivery schedule
Project documentation requirements
Special Requirements
Required pressure-vessel code
Inspection or third-party requirements
Special coating or color
OEM branding
Custom nozzle or mounting arrangement
Project Workflow
From RFQ to Air Receiver Supply
For custom and export projects, establishing the technical requirements before production helps avoid changes later in the manufacturing process.
Application Review
Compressor flow, pressure, demand profile and installation requirements are reviewed.
Technical Confirmation
Capacity, orientation, connections, materials and required project documentation are defined.
Manufacturing
The receiver is manufactured according to the agreed technical specification and production scope.
Inspection & Delivery
Agreed inspection, documentation and shipment requirements are completed according to the order scope.
Common Questions
Air Receiver Tank FAQ
Practical answers to the questions commonly raised when specifying an industrial air receiver tank.
What is an air receiver tank used for?
An air receiver stores compressed air and adds volume to the compressed air system. It helps cover short periods of high demand, reduces rapid pressure changes and provides a buffer between compressor output and downstream consumption.
Does every air compressor need a receiver tank?
The amount of external storage required depends on the compressor type and system design. Industrial systems with fluctuating demand generally benefit from adequate receiver capacity because additional system volume improves pressure response and provides reserve air.
How do I calculate the correct air receiver size?
Start with compressor airflow, the required storage time and the allowable pressure drop. Compressor control method, existing system volume, peak demand and piping losses should then be considered before selecting the final tank capacity.
Is receiver size based on compressor horsepower?
Horsepower can indicate the general size of a compressor, but it should not be the only sizing criterion. Actual delivered airflow and the plant's demand profile provide more useful information for selecting storage capacity.
What is the difference between a wet and dry air receiver?
A wet receiver is normally installed before the compressed air dryer and stores untreated compressed air. A dry receiver is generally installed after air treatment and stores dried, filtered air for downstream use.
Should I choose a vertical or horizontal air receiver?
A vertical receiver is usually preferred when floor space is limited. A horizontal receiver may be more suitable when installation height is restricted or when the tank needs to be integrated into an OEM or skid-mounted system.
Can an air receiver reduce compressor energy use?
Additional storage can improve compressor operating behavior in some systems by reducing rapid pressure changes and unnecessary cycling. Energy performance still depends on compressor controls, pressure settings, demand, air leaks and distribution-system efficiency.
Does an air receiver remove moisture?
An air receiver is not a substitute for an air dryer. Some moisture may condense as compressed air cools inside the tank, but applications requiring controlled air quality still need appropriate drying and filtration equipment.
Where should an air receiver be installed?
The correct location depends on the required function. A receiver can be installed before the dryer, after the dryer or near equipment with high intermittent demand. Large systems may use receivers in several locations.
Can an air receiver solve low-pressure problems?
It can help when the pressure drop is caused by short-duration demand that exceeds available instantaneous airflow. It will not solve continuous compressor undersizing, excessive leaks, blocked filters or severely undersized piping.
Can AIRNOVEX manufacture custom air receiver tanks?
AIRNOVEX can review custom capacity, orientation, connection arrangement, supports, surface treatment and OEM requirements. Final manufacturing details depend on the approved technical specification and required project standards.
Can I buy an air receiver together with a complete compressed air system?
Yes. AIRNOVEX supplies air receivers together with screw air compressors, variable speed air compressors, air dryers, filters and other industrial compressed air system components according to project requirements.
What information should I provide to an air receiver manufacturer?
Provide the required capacity if known, compressor airflow, operating pressure, maximum pressure, preferred orientation, connection sizes, quantity, destination country and any required pressure-vessel standard or inspection requirement.
AIRNOVEX INDUSTRIAL AIR SOLUTIONS
Specify the Right Air Receiver for Your Compressed Air Project
Send AIRNOVEX your compressor airflow, operating pressure, required storage capacity and installation requirements. If the receiver size has not yet been determined, provide the compressor data and air-demand information so the required configuration can be reviewed.
Standard and custom vertical air receivers, horizontal air receivers and OEM compressed air storage solutions are available for industrial projects.